FunctionChip fibrising at high temperature & pressure (mechanical pulp)
Key partsPlug screw / fillings / cartridge bearing unit / mechanical seal
Rotor mountingHydraulic drive-up, ≈ 200 bar final
1 · Equipment Overview
| Function | Chips softened in the preheater are fibrised between refining discs. |
| Plug screw | Conveys chips and forms the plug sealing the cooking zone. |
| Fillings | Balanced rotor fillings + non-balanced stator fillings. |
| Bearing unit | Cartridge type, replaced as a unit; joint sealed with liquid gasket. |
2 · Maintenance Process
PreparationRetract rotor; open bottom valve; shut water / steam; disconnect seal hoses.
Remove filling seatsUnbolt seat bolts; lift rotor / stator seats together with lifting tool.
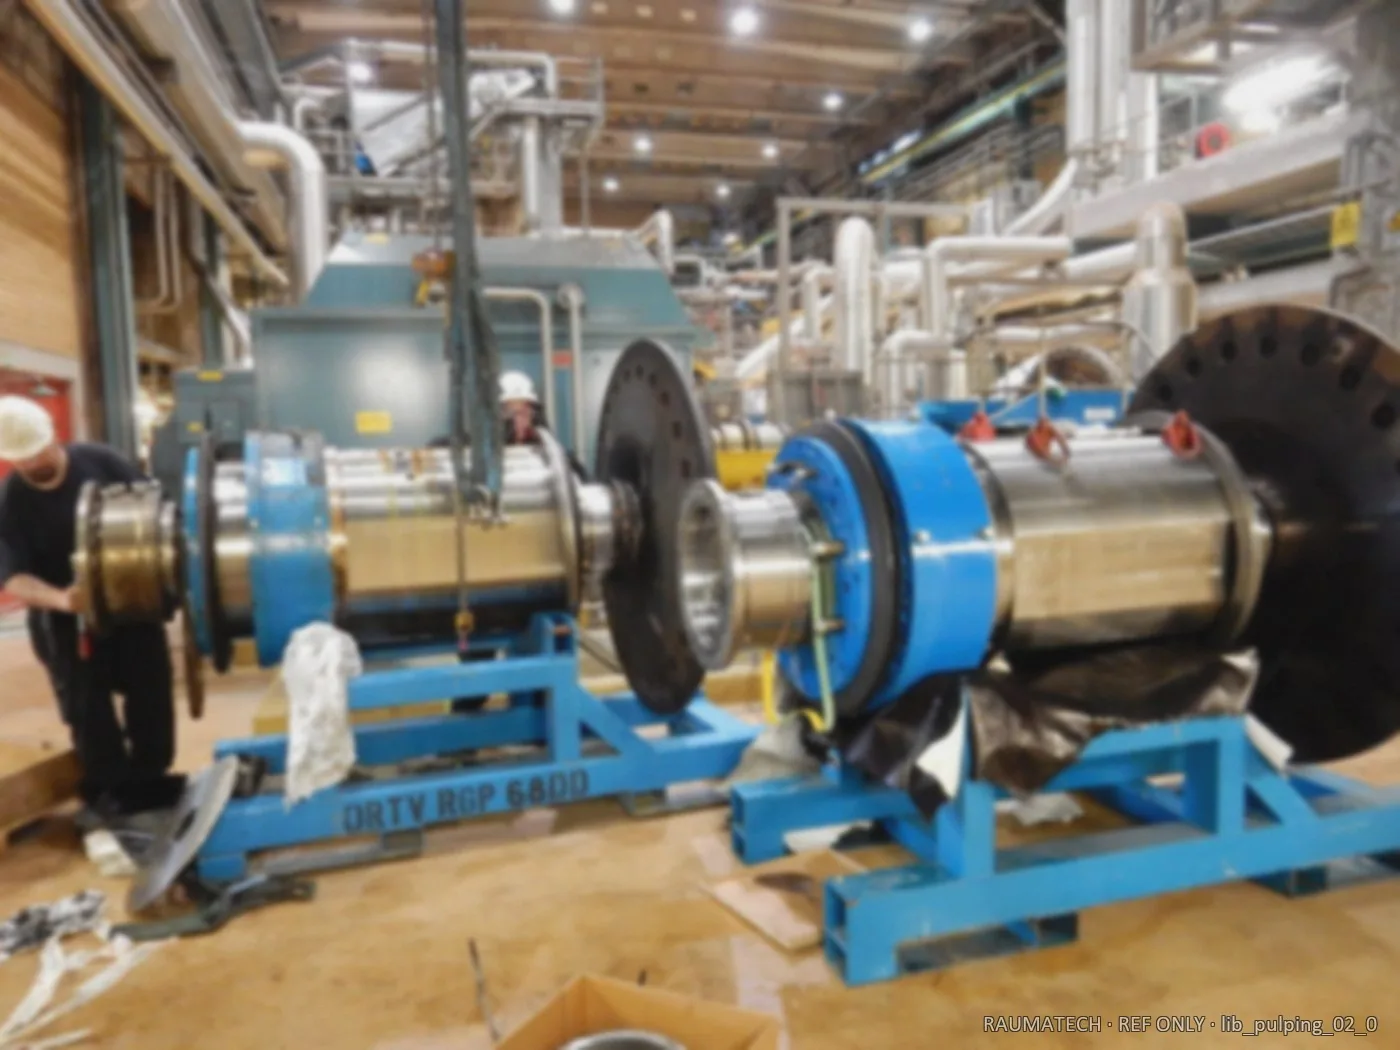
Remove rotorMark radial position; inject oil between rotor and shaft with HP pump; pull rotor with hydraulic nut. Initial 50–100 bar; ≈ 200 bar final mounting pressure
Mechanical sealRemove front-cover screws; inject HP oil between shaft and seal; slide out old seal; oil and fit new seal.
Bearing unitUnbolt mounting plate; lift out cartridge unit; clean faces and apply liquid gasket.
Filling renewalFit new fillings on the seats; clean refining-zone faces with non-abrasive tools.
Rotor refitOil the taper with ISO VG68; drive-up mount; after face contact apply +50 bar.
AlignmentDial-indicate rotor–stator alignment; adjust with wedge blocks and spring preload; re-check after several travels.
Flush & ventHot-oil flush of bearing unit (no cooling water); vent seal-water circuit; verify flow.
Trial runJog → ramp up; vibration spectrum on bearings; refit filling seats.
3 · Key Process Photos
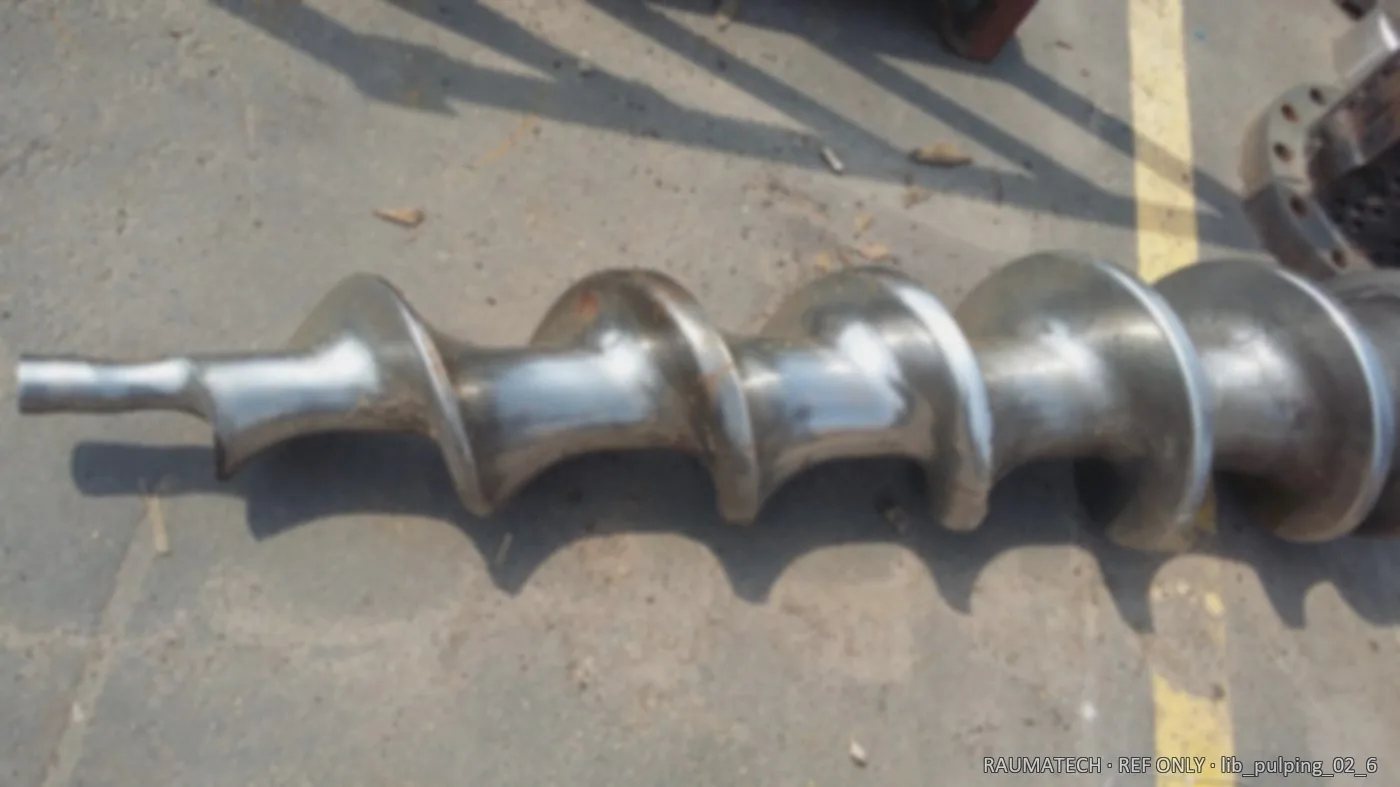
4 · Acceptance & Handover
Rotor drive-up mounted at ≈ 200 bar final pressure; rotor–stator alignment within tolerance; mechanical seal vented and leak-free; bearing unit gasket-sealed and hot-oil flush passed; fillings seated; trial vibration spectrum normal.